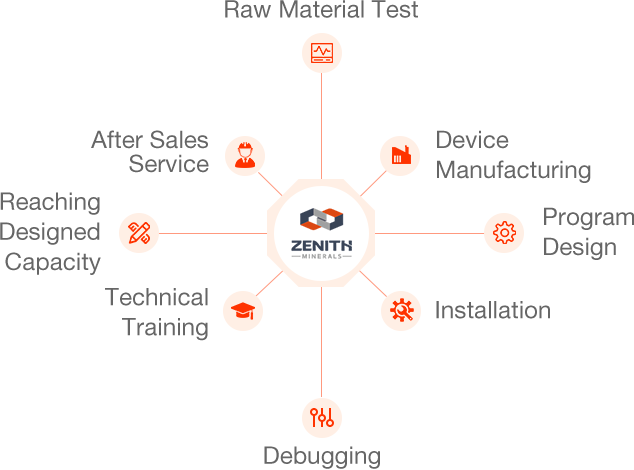
Zenith gains in-depth insights into the raw material characteristics and process requirements of various activated carbons, and optimizes grinding processes and equipment configurations in a targeted manner. It delivers end to end solutions that can be rapidly deployed and cover full production scenarios.
With precise process design, well reasoned equipment selection and intelligent control systems, efficient, stable and eco-friendly production of activated carbon powder is fully achieved.
Against the backdrop of accelerated development of the global environmental‑protection industry, activated carbon is embracing unprecedented development opportunities. Policies including China’s Action Plan for Water / Air Pollution Prevention and Control and the EU Industrial Emissions Directive have kept raising regulatory requirements, which strongly drives the rigid demand for high performance activated carbon in VOCs treatment and advanced wastewater treatment across printing dyeing, chemical, pharmaceutical, petrochemical and coating industries.
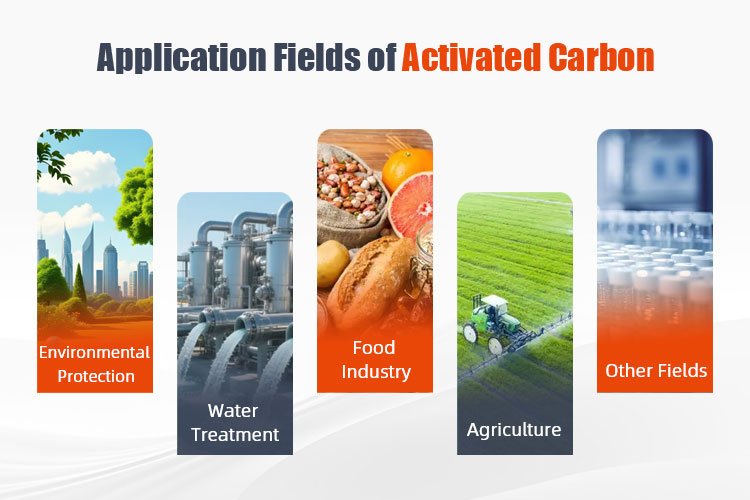
Meanwhile, its application scenarios are rapidly expanding into new energy, high end food & beverage, pharmaceutical purification and other fields, with continuously rising requirements for activated carbon performance and quality.
Activated carbon is a porous adsorbent material with abundant pore structure and high specific surface area. It is produced from raw materials such as coal, wood, fruit shells and synthetic resins via high temperature thermal treatment processes including carbonization and activation.
Classified by raw material sources, activated carbon is mainly divided into four categories: coal based, wood based (including coconut shell, fruit shell and wood chips), pitch based and synthetic resin based. Among them, coal based and wood based activated carbons occupy a dominant market position thanks to readily available raw materials, stable performance and controllable costs.
In terms of product forms, activated carbon falls into two major types: powdered and granular. Although powdered and granular activated carbon differ in final form and application scenarios, the grinding process is indispensable for the production of both, functioning at respective production stages.
Particle size control is directly related to reaction efficiency, adsorption performance and downstream adaptability. Therefore, a scientific, stable and controllable grinding system has become a core measure for enterprises to improve product quality and market competitiveness.
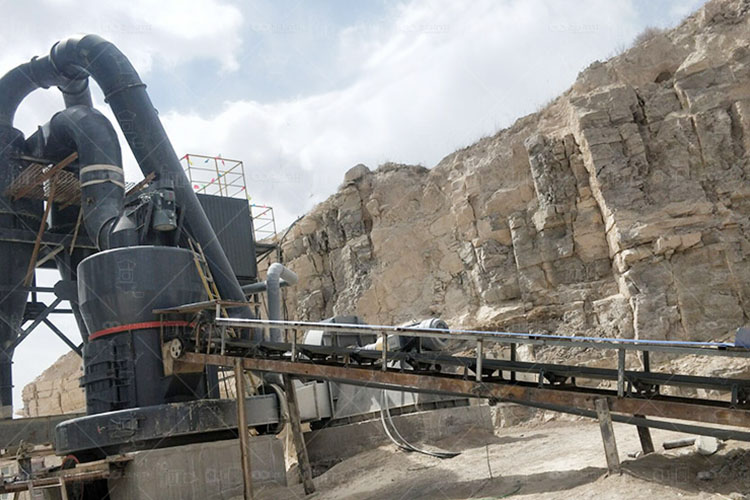
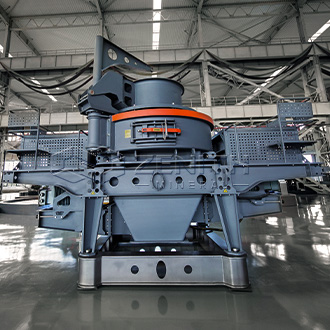
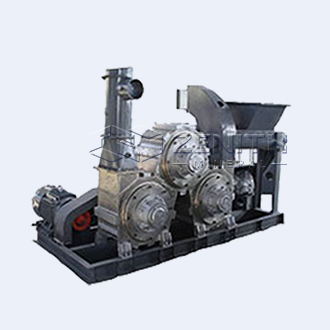
Centered on the core principles of “scenario-adaptation, cost reduction & efficiency improvement, and environmental compliance”, Zenith leverages its two flagship grinding mill series LM and MTW, together with nearly four decades of global project experience, to delve deep into application scenarios within the activated carbon industry. Through customized solutions based on LM and MTW series mills, Zenith provides the industry with stable and reliable grinding equipment support.
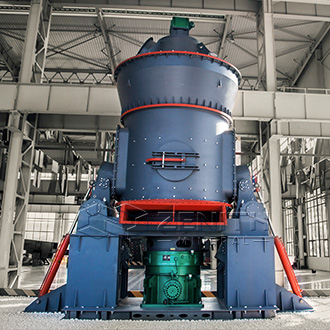
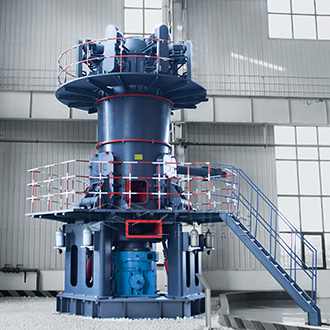
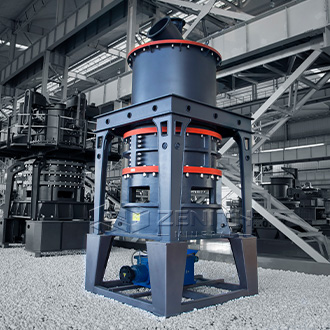
LM Vertical Roller Mill
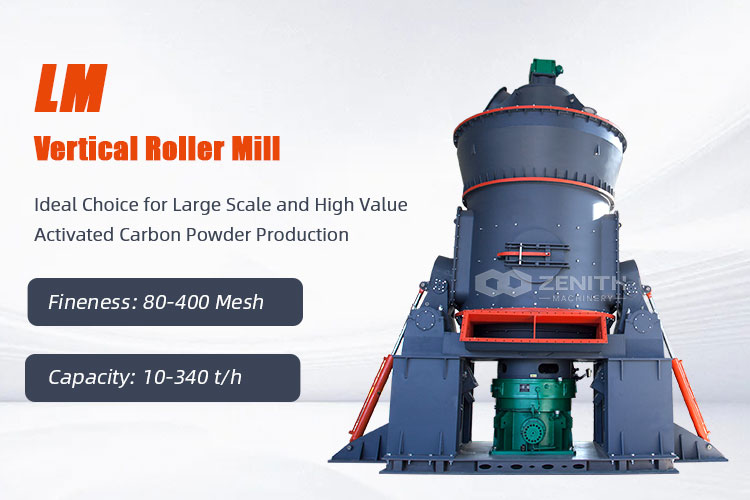
Product Advantages
Integrates crushing, grinding, drying, classification and conveying into one single unit.
Larger grinding area delivers high grinding efficiency.
Adopting specially designed roller and table structure, the grinding rollers are equipped with hydraulic automatic pressurizing devices.
Fitted with automatic control system for simple and flexible operation and lower operation and maintenance costs.
Fully sealed and operates under negative pressure with zero dust leakage.
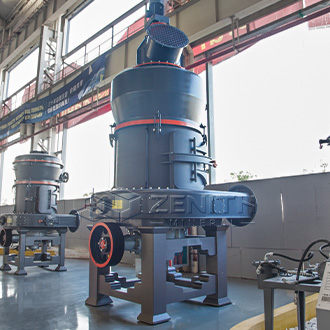
MTW European Trapezium Mill
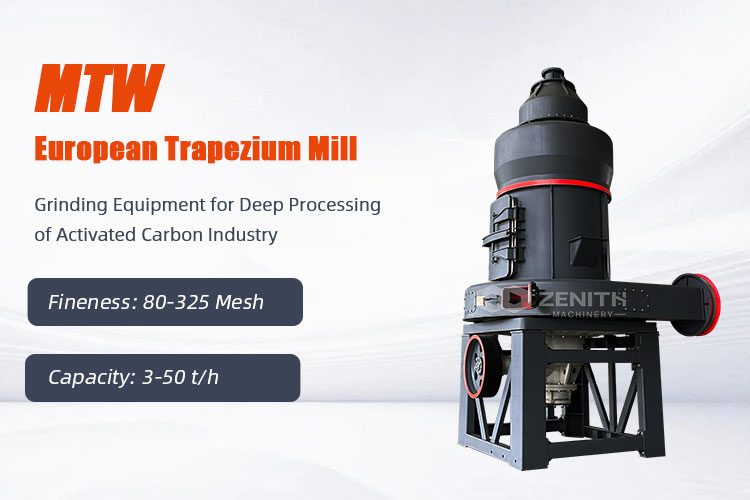
Product Advantages
Adopts curved shovel blade design to enlarge material grinding area and improve grinding efficiency with lower energy consumption.
It features integrated bevel gear transmission and resistance free air inlet volute design for better material flowability.
Low running resistance keeps oil temperature low.
The oil change interval can reach up to 4 months with less frequent maintenance.
Zenith equipment is exported to more than 180 countries and regions worldwide. In the activated carbon sector, our equipment covers multiple segmented application scenarios, consistently achieving the core objectives of “qualified product quality, improved efficiency and environmental compliance”. Our equipment reliability and service response speed have won high recognition from customers.